

 Contact Us
Compact Power for Conveyor Automation
Looking for the right motors to power your conveyor systems? Dunkermotoren offers high-performance BLDC motors, brushed motors, and linear motors built for reliability and precision in food and beverage production.
- Hygienic Design and Cleanability:
Stainless steel housings and up to IP69K protection ensure easy cleaning and washdown suitability. - Compact and Robust Construction:
Our compact, durable motors fit into tight spaces and perform reliably in demanding production environments. - Integrated Intelligence and Connectivity:
With built-in electronics and support for PROFINET, EtherCAT, and other interfaces, our motors integrate seamlessly into modern automation systems. - Reduced Maintenance with nexofox:
nexofox enables predictive maintenance to reduce downtime and extend service life.
Your Conveyor Challenge, Our Drive Solution
In the food and beverage industry, conveyor systems meet strict hygiene standards, operate reliably under demanding conditions, and integrate seamlessly into complex production environments. At Dunkermotoren, we offer tailored drive solutions and expert support to help you meet these challenges with confidence.
- Hygienic and Application-Specific Design:
Our motors are engineered for hygienic environments, featuring stainless steel housings, smooth surfaces, and protection classes up to IP69K. We offer solutions for temperature-sensitive zones, sticky or delicate products, and support the use of FDA- and EU-compliant materials. - Advanced Conveyor Integration:
Dunkermotoren drives support a wide range of conveyor technologies, including spiral, vacuum, and magnetic conveyors. We enable optimized product flow through integration with diverters, sorters, pushers, and accumulation zones. Ideal for dynamic production line. - Smart Automation and Control:
With integrated electronics and interfaces like PROFINET, Ethernet/IP, CanOpen and EtherCAT, our drives connect easily to SCADA, MES, and robotic systems. We also support zone-based conveyor control and sensor integration for tracking, weighing, and filling.


Get a free consultation to discuss your specific needs and find the best solution for your application.
Motors for Conveyor Applications
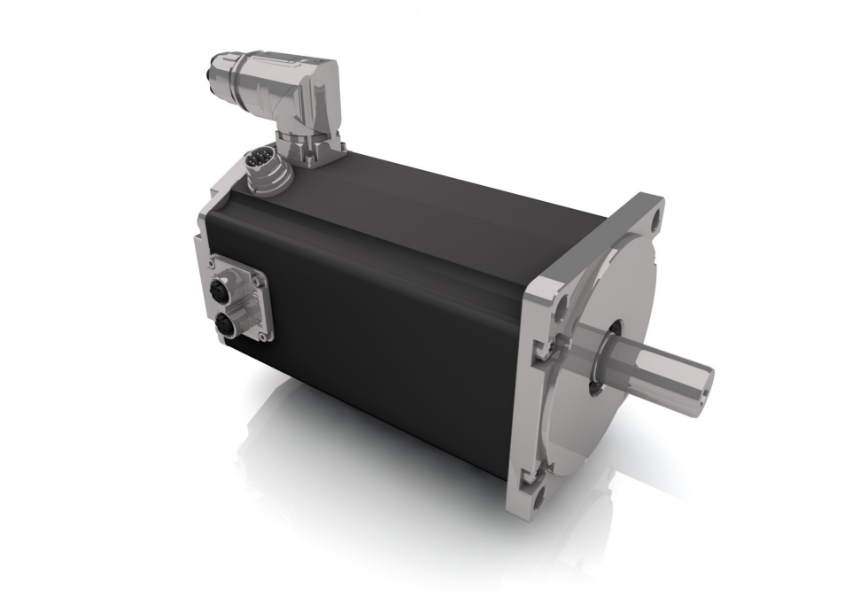
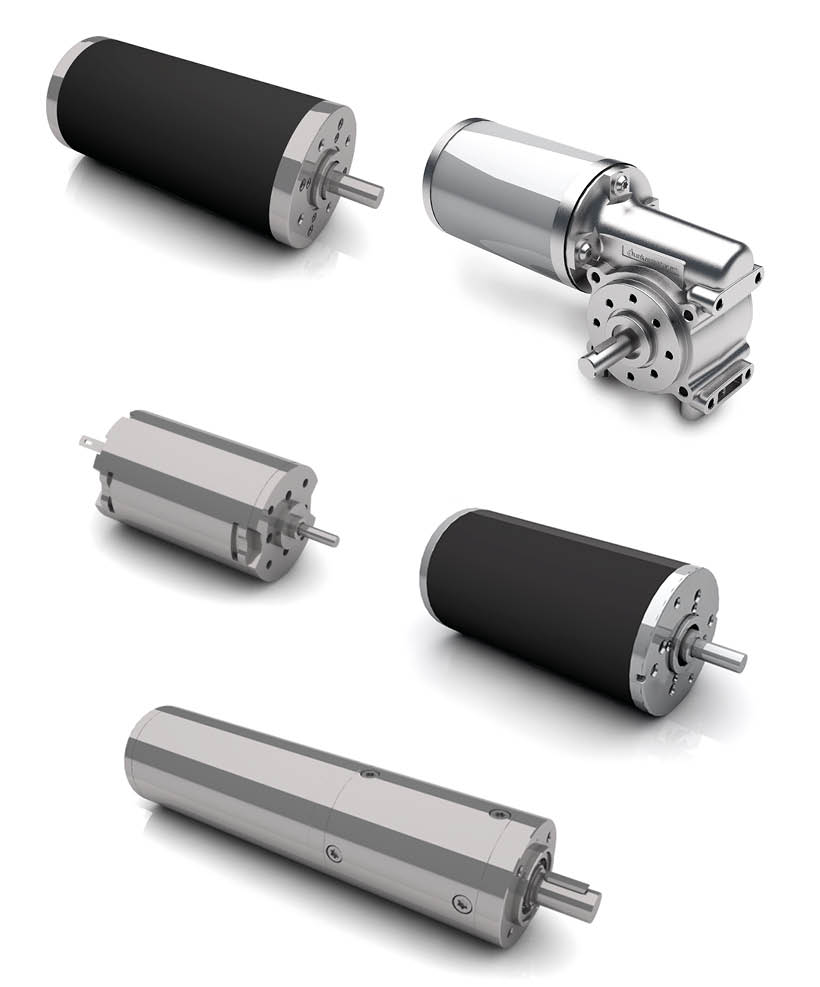
Powering Conveyor Systems in Food Production
From portioning to packaging, conveyor systems are key to efficient food and beverage production. Dunkermotoren motors support these processes with reliable performance, hygienic design, and easy integration. The following applications show how our drive solutions contribute to smooth and precise operation across various conveyor types.
Bottle Transport and Crate Loading System
Smooth bottle transport is essential for efficient packaging in the food and beverage industry. Whether moving filled or empty bottles through sorting, inspection, or final packaging, these systems demand precise synchronization, gentle handling, and hygienic operation. Our motors ensure controlled movement and accurate positioning, helping prevent damage and enabling reliable crate placement. Thanks to their compact design and smart connectivity, they integrate seamlessly into automated filling and packaging lines.
Talk To An Expert
Trough Chain Conveyor
Trough chain conveyors are designed for the horizontal or slightly inclined transport of heavy or bulky materials such as grains, malt, or flour. These systems require powerful and durable drive solutions that can operate reliably over long distances and under continuous load. Dunkermotoren BLDC gear motors provide the necessary torque and endurance to ensure smooth, uninterrupted material flow. Their robust design and high efficiency make them ideal for demanding food production environments where reliability is critical.
Talk To An Expert
Bucket Elevator
Handling bulk materials efficiently requires reliable vertical transport solutions. Bucket elevators are used for vertical transport of bulk materials like sugar, coffee beans, or powdered ingredients, often with high throughput rates. These systems demand precise lifting and controlled discharge to maintain product integrity and process efficiency. Motor Solutions from Dunkermotoren deliver consistent performance and accurate speed control, ensuring smooth elevation and gentle handling. Their compact design and integration flexibility make them a perfect fit for silo filling, packaging lines, and vertical conveying in hygienic zones.
Talk To An Expert
Hygienic Screw Conveyor
Hygienic screw conveyors are essential for transporting sensitive or regulated food products in environments that demand full compliance with hygiene standards. Constructed from stainless steel and designed for easy cleaning, these conveyors are used in applications like dairy, baby food, or ready-to-eat meals. Dunkermotoren motors meet FDA and EU food-grade standards and are available in various sizes for fast integration. Their sealed design and high ingress protection ensure safe operation in washdown zones and cleanroom conditions.
Talk To An Expert
Other Conveyor Systems where Dunkermotoren are used
Spiral Conveyor
Spiral conveyors gently transport lightweight materials like tea leaves or spices. Our compact motors ensure smooth, space-saving movement with minimal product stress.
Tube Screw Conveyor
Tube screw conveyors are used for short-distance transport of powders or granules. Dunkermotoren motors deliver efficient, reliable drive performance in compact system layouts.
Modular Belt Conveyor
Designed for hygienic environments like bakeries or dairy plants, modular belt conveyors move packaged goods or trays with precision. Our motors provide clean, consistent drive performance with minimal maintenance.
Benefits of our Motors in Food & Beverage Conveyor Systems
Our motors are engineered to enhance the performance, hygiene, and efficiency of conveyor systems in demanding food and beverage environments:
- Hygienic Design: Stainless steel housings and IP69K protection enable thorough cleaning and resistance to harsh cleaning agents, supporting compliance with strict hygiene standards.
- Precise Product Handling: High positioning accuracy and integrated control electronics ensure smooth and consistent transport of food items, reducing waste and improving process reliability.
- Energy Efficiency: Motors with up to IE4 efficiency help lower energy consumption and support sustainability targets in continuous production environments.
- Minimal Maintenance: Sealed and robust motor designs allow for 24/7 operation with reduced service intervals, keeping conveyor systems running reliably.
- Real-Time Monitoring: Live performance data supports proactive maintenance and process optimization, reducing the risk of unexpected downtime.
- Integrated Safety Functions: Features like Safe Torque Off (STO) enable safe operation in automated environments, protecting both equipment and personnel.